Veikong Electric

Author: Veikong Electric

why motor cable length matters in VFD systems, with reflected voltage and output protection highlighted.

Why Does Motor Cable Length Matter in VFD Systems? Understanding Reflected Voltage and Output Protection

When installing a variable frequency drive, engineers often pay close attention to the motor power, voltage, current, and load type. However, the distance between the VFD and the motor is sometimes treated as a secondary detail.  In reality, motor cable length can significantly affect the electrical behavior of a VFD system. When the cable becomes long, the motor terminals may experience higher voltage stress, increased electromagnetic interference, leakage current, and other problems that are not obvious from the motor nameplate.  Understanding these effects can help engineers select suitable cables, plan the installation correctly, and determine whether an output reactor, dV/dt filter, or sine wave filter is required.  Why Is a VFD Output Different from a Normal Power Supply?  A VFD does not produce a perfectly smooth sinusoidal voltage directly. Its power semiconductors switch the DC bus voltage rapidly to create a pulse-width-modulated output, commonly known as PWM.  The motor current may remain relatively smooth because the motor windings have inductance. However, the voltage waveform traveling through the cable consists of fast switching pulses with steep voltage edges.  When the VFD is installed close to the motor, these pulses usually reach the motor with limited cable-related distortion. As the cable becomes longer, its electrical characteristics become more important. The cable begins to behave like a transmission line rather than a simple conductor.  How Does Reflected Voltage Occur?  The VFD cable and motor do not always have the same electrical impedance. When a fast voltage pulse reaches the motor terminals, part of the pulse may be absorbed by the motor, while another part may be reflected toward the drive.  The reflected pulse can combine with the incoming pulse and temporarily increase the voltage at the motor terminals. This phenomenon is often called reflected-wave voltage or reflected voltage.  The amount of voltage stress depends on several factors, including cable length, cable type, motor impedance, system voltage, PWM rise time, carrier frequency, grounding, and motor insulation design. Therefore, there is no single cable length that is considered “long” for every VFD installation.  Repeated voltage peaks may gradually weaken motor winding insulation. Older motors or motors not designed for inverter operation may be more sensitive to this stress, especially in higher-voltage systems.  What Other Problems Can Long Motor Cables Cause?  Reflected voltage is not the only concern. A long cable also introduces additional capacitance between phases and between the conductors and ground.  Every time the VFD output switches, this capacitance must be charged and discharged. The resulting high-frequency current can increase stress on the drive output, contribute to leakage current, and create electromagnetic interference.  Possible symptoms include:  These symptoms do not automatically prove that cable length is the only cause. Grounding, shielding, motor condition, parameter settings, cable routing, and installation quality should also be checked.  How Should Motor Cables Be Installed?  Cable selection and installation are the first line of protection. A cable suitable for inverter duty is generally preferred, particularly when the motor cable is long or the surrounding environment is sensitive to electrical interference.  The cable shield should be properly terminated according to the system design. Ground connections should be short, secure, and designed to provide a low-impedance path for high-frequency current.  Motor cables should be separated from signal cables, encoder cables, communication wiring, and low-voltage control circuits. If power and signal cables must cross, crossing them at approximately 90 degrees can help reduce interference.  The cable route should also be planned carefully. Coiling unnecessary cable length can increase inductive and capacitive effects and should generally be avoided.  When Is an Output Reactor Used?  An output reactor is installed between the VFD and the motor. It adds inductance to the output circuit and can reduce current ripple, limit rapid current changes, and decrease some of the electrical stress caused by the cable.  For moderate cable lengths, an output reactor may provide sufficient improvement. It can also help protect the drive when the motor or cable creates a demanding output condition.  However, an output reactor does not produce a sinusoidal waveform and may not fully control reflected voltage in every long-cable application. Its suitability should be evaluated according to the VFD, motor, cable length, voltage level, and operating frequency.  What Is the Difference Between a dV/dt Filter and a Sine Wave Filter?  A dV/dt filter is designed to reduce the rate of voltage change and limit voltage peaks reaching the motor. It is commonly considered when motor cable length or motor insulation stress exceeds what can be handled by basic output protection.  A sine wave filter provides a higher level of filtering. It converts the PWM output into a waveform that is much closer to a sinusoidal voltage before it reaches the motor.  Sine wave filters may be used for very long motor cables, sensitive motors, applications requiring lower motor noise, or installations where the motor is located far from the control equipment. They are larger and more expensive than output reactors and must be correctly matched to the VFD and operating frequency.  How Should Engineers Evaluate a Long-Cable Application?  Before installation, engineers should confirm:  The VFD manufacturer’s cable-length recommendations should always be reviewed. If the application exceeds the recommended conditions, the appropriate output protection should be confirmed before commissioning.  Applying VEIKONG VFDs in Long-Cable Systems  VEIKONG provides variable frequency drives for pumps, fans, compressors, lifting equipment, production machinery, and other industrial applications.  When applying a VEIKONG VFD in a system with a long motor cable, customers should provide the motor parameters, voltage, cable length, application type, and installation conditions. Our sales and engineering teams can help evaluate the application and determine whether additional output protection should be considered.  Correct cable planning and output protection can reduce electrical stress, improve motor reliability, minimize interference, and support more stable operation throughout the service life of the system. 
Read More »
Veikong VFD technical insight explaining why a variable frequency drive can overheat when motor current is normal, highlighting carrier frequency, heat, and derating.

Why Can a VFD Overheat Even When the Motor Current Is Normal? Understanding Carrier Frequency, Ambient Temperature

When a variable frequency drive reports an overtemperature alarm, the first reaction is often to check whether the motor current has exceeded the VFD’s rated current.  High output current can certainly increase heat generation. However, a VFD may still overheat even when the displayed motor current appears normal. This is because the drive’s internal temperature is affected by many factors other than motor current.  Carrier frequency, ambient temperature, cabinet ventilation, cooling fan condition, dust accumulation, installation spacing, altitude, and load cycle can all influence the temperature of the power components.  Understanding these factors helps engineers identify the real cause of overheating instead of simply replacing the VFD with a larger model.  Where Does Heat Inside a VFD Come From?  A VFD contains rectifier components, a DC bus, capacitors, power semiconductor modules, control circuits, and cooling components.  During operation, current passing through the rectifier and power modules creates conduction losses. At the same time, the output semiconductor devices switch on and off rapidly to generate the PWM waveform required to control the motor.  Every switching event produces a small amount of energy loss. The heat generated by a single event may be limited, but thousands of switching events occur every second. The accumulated switching loss can therefore become an important part of the VFD’s internal heat.  Additional heat may also come from the charging circuit, DC bus components, internal braking unit, control power supply, and surrounding equipment inside the electrical cabinet.  Why Does Carrier Frequency Affect VFD Temperature?  Carrier frequency determines how frequently the VFD’s output semiconductor devices switch.  A higher carrier frequency can reduce audible motor noise and may improve the smoothness of the motor current waveform. For this reason, some users increase the carrier frequency when the motor produces an obvious high-frequency sound.  However, increasing the carrier frequency also increases the number of switching events per second. More switching events generally mean higher switching losses and additional heat inside the VFD.  The motor current may remain below the rated value while the VFD temperature continues to rise. In this situation, the current display alone does not show the complete thermal condition of the drive.  Carrier frequency should therefore be selected according to the motor, application, cable length, noise requirements, ambient temperature, and VFD manufacturer’s recommendations. Setting it unnecessarily high may reduce the available output capacity or require derating.  How Does Ambient Temperature Affect Cooling?  A VFD transfers heat from its power components to a heat sink and then releases that heat into the surrounding air.  If the air entering the VFD is already hot, the temperature difference between the heat sink and the surrounding environment becomes smaller. The cooling system can no longer remove heat as effectively.  This situation is common in enclosed control cabinets, outdoor installations exposed to sunlight, factories with ovens or heating equipment, and environments where several high-power devices are installed close together.  The temperature inside an electrical cabinet can be significantly higher than the room temperature. Measuring only the workshop temperature may therefore lead to an incorrect conclusion. The temperature should be checked near the VFD’s air inlet under actual operating conditions.  Why Is Cabinet Ventilation Important?  A cooling fan can move air only when there is a clear path for airflow. If the cabinet inlet, outlet, filter, or VFD air duct is blocked, hot air may circulate inside the cabinet instead of being discharged.  Common installation problems include:  In dusty environments, filters and heat sinks require regular inspection and cleaning. A filter may appear acceptable from the outside while its internal airflow has already been significantly reduced.  Can a Cooling Fan Cause Intermittent Overheating?  Yes. A cooling fan may still rotate but no longer provide sufficient airflow because of bearing wear, dust, reduced speed, or unstable power supply.  This can create intermittent overheating. The VFD may operate normally when the load or ambient temperature is low but report an overtemperature alarm during longer production cycles or warmer periods.  Maintenance personnel should check not only whether the fan rotates, but also whether the airflow is strong and stable. Fan operating time and replacement recommendations should also be considered.  Why Does Altitude Require Derating?  At higher altitudes, air density decreases. Lower air density reduces the amount of heat that can be removed by the same airflow.  Even if the ambient temperature is not particularly high, a VFD operating at high altitude may have lower cooling capacity than the same model installed near sea level.  The insulation and cooling requirements of electrical equipment can also change with altitude. When an installation exceeds the manufacturer’s standard operating altitude, the applicable derating requirement should be confirmed.  What Does VFD Derating Mean?  Derating means operating the VFD below its nominal output capacity when environmental or operating conditions are more demanding than the standard rated conditions.  Derating may be required because of high ambient temperature, high altitude, elevated carrier frequency, demanding load cycles, or installation inside a poorly ventilated cabinet.  For example, a VFD with a certain rated current under standard conditions may need to operate at a lower continuous output current in a hot environment. Alternatively, a higher-power VFD may be selected to provide sufficient thermal margin.  Derating is not an indication that the VFD is defective. It is an engineering method used to maintain reliability and service life under non-standard conditions.  How Should an Overheating Problem Be Investigated?  When a VFD reports an overtemperature alarm, engineers should check:  The alarm history should also be reviewed. If overheating occurs only at a particular time of day, production stage, or load condition, that pattern may help identify the cause.  Using VEIKONG VFDs in High-Temperature Applications  VEIKONG provides VFD solutions for a wide range of industrial motor applications. Correct selection, installation, ventilation, parameter settings, and maintenance are essential for reliable operation.  For applications involving high ambient temperatures, enclosed cabinets, high altitude, elevated carrier frequency, or continuous heavy loads, customers should provide the relevant operating conditions during product selection.  VEIKONG’s sales and engineering teams can help evaluate the application, recommend a suitable

Read More »
Maximizing ROI in Agriculture

Maximizing ROI in Agriculture: The Complete Guide to Solar Pump Inverters

Water is the single biggest variable in farming. Too little, and crops fail. Too much costs to pump it, and margins disappear. For decades, farms without grid access leaned on diesel generators to keep water moving, accepting the fuel bills, the noise, and the constant maintenance that came with them.  Solar-powered pumping has changed the math. Falling solar panel costs, paired with smarter control electronics, now let farms pump water straight from sunlight, with no fuel truck and no diesel engine to service.  But the panels are only half the story. The part that actually makes a solar pumping system work well, day after day, season after season, is the inverter that sits between the panel and the pump.  This guide breaks down what a solar pump inverter does, how it protects your equipment, and what to look for if you’re trying to get the most return out of a solar irrigation investment.  What Is A Solar Pump Inverter?  A solar pump inverter, also called a solar variable frequency drive (VFD), converts the direct current (DC) coming from solar panels into alternating current (AC) that a water pump motor needs to run.   It’s the component that lets a solar array actually drive real farm equipment, such as centrifugal pumps, irrigation pumps, deep well pumps, and even swimming pool pumps.  Depending on the model, these inverters accept a solar DC input in the 160-450VDC or 350-800VDC range, and many can also run on a three-phase AC supply (220V, 380V, 400V, 460V, or 480V) or single-phase power.   That flexibility matters on a farm, where you might have grid power at one plot and none at another.  How the System Works Without a Battery  Most off-grid solar setups need a battery bank, which adds cost and another part that eventually wears out. A solar pump inverter skips that step entirely.   As long as there’s sunlight, it can generate load independently. In place of a battery, it uses a water level control system to manage supply, and it adjusts its output frequency in real time based on how strong the sunlight is.  This is where the built-in maximum power point tracking (MPPT) system earns its keep. MPPT constantly finds the best possible power output from the solar array, so the pump gets the most usable energy the panels can produce at that moment, whether it’s full midday sun or a cloudy morning.  The ROI Case: Why Solar Pump Inverters Pay for Themselves  The return on investment for a solar pump inverter comes from three places: what you stop spending, what you stop losing to downtime, and what you get out of the same solar array.  Put together, those savings are what let a solar pump inverter earn back its upfront cost faster than most farms expect, especially in areas where diesel has to be trucked in.  Features That Protect the Investment  A cheap inverter that fails in year two erases any ROI advantage. The features below are what keep a solar pumping system running for its full working life.  1. Maximum Power Point Tracking (MPPT)  MPPT is the core of any solar pump inverter’s efficiency. On Veikong’s VFD500-PV and VFD510-PV models, average MPPT tracking efficiency is rated at 99.5% or higher, with the VFD500-PV listed as reaching up to 99.9999% MPPT efficiency in both static and dynamic conditions. In plain terms, the inverter wastes almost none of the power your solar array produces.  2. PID Function Within MPPT Mode  Both product lines also run a PID (proportional-integral-derivative) function inside MPPT mode, which helps keep pump pressure and flow steady even as sunlight conditions shift throughout the day.  3. Dry Run and Water-Level Protection  Running a pump dry can burn out a motor fast. Veikong’s solar pump inverters include dry-run protection, along with full-water and low-water detection, so the pump shuts down automatically before it damages itself. A “wake up and sleep” function also lets the system power down and restart on its own as water levels change.  4. Hybrid AC and DC, With Auto Switching  Because these inverters support both solar DC input and AC grid input, and can switch automatically between the two, a farm isn’t left without water on a heavily overcast day if grid power is available as backup.  5. Remote Monitoring  Veikong’s VFD500-PV includes a built-in S200-GPRS module for remote monitoring. From a PC, users can track flow speed, daily flow volume, current power output, and total generation without needing to physically check the pump site. Both the VFD500-PV and VFD510-PV also offer optional LCD keypads and optional GPRS remote control, and the VFD510-PV’s keypad is available in English or Arabic.  6. Motor Compatibility  The inverters support both induction motors (IM) and permanent magnet synchronous motors (PMSM), and work with surface-mount pumps as well as submersible pumps, which covers most farm pump setups without needing custom equipment.  Choosing the Right Model for Your Farm  Not every plot needs the same inverter. Here’s how Veikong’s two main solar pump inverter lines compare, based on their published specifications.    VFD500-PV  VFD510-IP55  Power range (220V)  0.75kW-110kW  2.2kW-11kW   Power range (380V)  0.75kW-710kW  2.2kW-45kW   Protection level   Standard enclosure   IP55, built for harsh environments   MPPT tracking efficiency   Up to 99.9999% (average ≥99.5%)  Average ≥99.5%   Keypad language   LCD keypad (optional)  LCD keypad, English/Arabic (optional)   Remote monitoring   GPRS via S200 module   Optional GPRS remote control    For large-scale irrigation or bigger wells, the VFD500-PV’s wider power range gives more headroom. For smaller or mid-sized pumping needs in dusty, humid, or otherwise harsh field conditions, the VFD510-PV’s IP55-rated enclosure is built specifically to handle that exposure.  Across both single-phase and three-phase configurations, Veikong’s solar pump inverter range spans 1kW to 710kW, which covers everything from a single small irrigation pump to a large agricultural well system.  Where Solar Pump Inverters Get Used on Farms  According to Veikong, its solar pump inverters are already deployed in:  Since the VFD500-PV line was released to the global market at the end of 2015, Veikong reports more than 1,000 successful installations across these

Read More »
Integrating VFDs into Smart Factories

Integrating VFDs into Smart Factories: A Technical Guide to Modbus and PLC Communication

Modern factories increasingly rely on equipment that can share data in real time. A pump reports back to the system managing the boiler. A crane’s motor sends load data to a control room on the other side of the plant.  This level of coordination is not accidental. It depends on two pieces of equipment that can exchange information in a common format. The first is the variable frequency drive, or VFD.   The second is the programmable logic controller, or PLC. When these two systems communicate reliably, a factory moves from operating as a set of independent machines to functioning as one coordinated system.  This guide explains how that connection works, which protocol makes it possible, and what to look for in a drive designed for this kind of integration.  What a VFD Actually Does   A variable frequency drive is an electronic system that controls an AC induction motor. It manages torque, speed, and direction, and it starts a motor smoothly instead of slamming it up to full speed. Instead of running a motor at one fixed speed off the power grid, a VFD lets you dial in exactly the speed a process needs, then change it on the fly.  A VFD system generally has three parts:  Modern drives have shrunk a lot over the years, mostly because microprocessors replaced older solid-state parts. That shrinkage matters for smart factories, because a smaller, smarter drive has more room left over for communication hardware.  Why Modbus Matters for VFD-PLC Communication  A smart factory needs its machines to report data and accept commands without a person standing at every panel. Modbus is one of the oldest and most widely used protocols for this job. It’s simple, it’s open, and most industrial equipment supports it in some form. That’s exactly why it shows up so often when a VFD needs to talk to a PLC.  In practice, Modbus lets a PLC read a drive’s status, like speed, fault codes, or temperature, and write new commands back, like a new target frequency or a start/stop signal. The PLC acts as the master, polling each drive on the network in turn.   This keeps wiring simple, since one communication cable can often replace a tangle of separate control wires running to every drive on the floor.  Communication Protocols Built Into Veikong Drives  Not every VFD is built with this kind of networking in mind. Veikong designs its higher-end AC drives specifically to plug into automated, PLC-driven environments.  1. VFD580: High-End Drive with Multi-Protocol Support  The VFD580 is Veikong’s high-standard vector inverter, built for applications that demand strong overall performance, including electromagnetic compatibility and scalability. On the communication side, it supports:  The drive also comes with a standard LCD that shows a real-time clock, supports multiple languages, and allows parameter upload and download, along with software upgrades.   It supports PC tool software for setup and diagnostics, so an engineer can configure the drive from a laptop instead of a keypad. For applications like pumps and fans, it includes an energy-saving function for light loads, and it supports SVC vector control and closed-loop vector control for high-precision work.  2. VFD530: Communication Built for Lifting and Precision Work  The VFD530 is Veikong’s high-performance PMSM AC drive, built on the VFD500 platform, meaning it inherits all of that series’ functions and adds more. Its communication feature set includes:  It also supports multiple PG cards and protocols, which matters for applications using encoder feedback. The drive runs on a 256K TI CPU, giving it faster response and higher precision, and it supports closed-loop PG card operation for both synchronous and asynchronous motors.  For lifting applications like hoists and cranes, it includes a special brake logic function and standard double relay output.  Built-In PLC Functionality: One Less Box to Wire  Here’s something that often gets missed when people plan a smart factory retrofit: some VFDs don’t just talk to a PLC; they can act like a small one.  Both the VFD580 and VFD530 include a built-in comparator and logic control unit that functions as a simple PLC. This means basic interlocks, threshold checks, and logic sequences can run directly inside the drive, without needing a separate controller for every small task.   For a factory floor with dozens of drives, this can cut down on the number of external PLCs needed just to handle simple logic, while the plant-wide PLC still handles the bigger picture through Modbus or another supported protocol.  The VFD530 adds double PID function support on top of this, useful for processes that need two independent control loops running at once, such as pressure and flow control on the same line.  Soft Starters Join the Network Too  VFDs aren’t the only piece of motor control equipment that needs to report into a PLC-based system. Veikong’s VKS8000 series bypass soft starter also supports Modbus communication, with optional TCP communication available.   It includes a built-in bypass contactor and a PT100 temperature sensor, so a PLC can monitor motor temperature alongside start and stop status through the same network used for the drives.  This matters in mixed environments, which are common. A factory rarely runs on VFDs alone. Large motors that only need a controlled start, rather than variable speed, are often paired with a soft starter instead. Having both device types speak the same protocol keeps the PLC program simpler and the wiring more consistent across the plant.  Where This Shows Up on the Factory Floor  Veikong’s drives are used across a range of industrial settings where speed control and network integration both matter:  In every one of these cases, the drive isn’t working alone. It’s reporting status and taking commands from a larger control system, which is exactly the role Modbus and PLC integration are built to support.  Quality Standards Behind the Hardware  Communication protocols only matter if the hardware behind them is reliable. Veikong follows the ISO9001 standard to manage and supervise product quality, and its products carry CE certification along with other technical approvals.   The company also states that its

Read More »
Variable Frequency Drive (VFD) vs. Soft Starter

Variable Frequency Drive (VFD) vs. Soft Starter: A Comparative Guide for Industrial Motor Control

Electric motors run the world’s factories, pumps, fans, and cranes. Starting a motor the wrong way can shorten its life, trip breakers, or waste energy every day. That’s why plant engineers often compare two common solutions: the variable frequency drive (VFD) and the soft starter.  Both devices control how a motor starts, but they do different jobs. Picking the wrong one can mean paying for features you don’t need, or missing you could have had.  This guide breaks down what each device does, where each fits best, and how to choose between them.  What is a Variable Frequency Drive (VFD)?  A VFD is an electronic system used to control an AC induction motor. It manages torque, speed, and motor direction, bringing the motor up to the desired speed at a controlled acceleration rate instead of starting it at full speed instantly.  Utility power runs at a fixed frequency. A VFD breaks that limit, letting one motor run at many different speeds so it can handle a variety of jobs without being oversized or underused.   A VFD system has three parts: an AC motor, usually three-phase; a main drive controller, solid-state electronics that convert power, including a filter, switch, and inverter section; and a control interface, used to start and stop the motor, adjust speed, and change direction.  Modern VFDs are far more compact than older models, mostly because microprocessors have replaced older solid-state components.  When Should You Use a VFD?  A VFD makes sense whenever a process needs more than a simple on/off start:  What Is a Soft Starter?  A soft starter solves a narrower problem: the harsh jolt a motor gets when switched on at full voltage. VEIKONG’s S6000 soft starter is an intelligent digital motor soft start system with a complete set of protection functions.  Instead of controlling speed continuously like a VFD, a soft starter ramps voltage up gradually, then runs the motor at full, fixed speed.   According to VEIKONG, this approach cuts system cost, extends equipment life, works as a modern alternative to the traditional star-triangle (wye-delta) starter and the self-coupling decompression starter, and improves system reliability.   Since it doesn’t manage speed after ramp-up, it’s a simpler, more affordable option for motors that only need to run at one speed.  Where Soft Starters Are Typically Used  VEIKONG lists general soft start applications anywhere traditional across-the-line or wye-delta starting would normally apply, including motor fans, compressors, crushers, transmission machines, pumps, and grinders.   For compressors, limiting startup current reduces abrasion and motor heat. For crushers, block protection stops the motor from being damaged during a jam. For pumps, controlled starting reduces water hammer, lowering maintenance costs.  VEIKONG’s soft starters also serve agitators, ball mills, centrifuges, chillers, conveyors, escalators, feeders, hammer mills, lathe machines, flour mills, mixers, pelletizers, plastic and textile machines, presses, rolling mills, saws, vibrating screens, transformers, tumblers, and wood chippers.  VFD vs. Soft Starter: The Core Differences  A soft starter manages the moment of startup. A VFD manages the motor’s entire operating life, from the first second to shutdown.  1. Speed Control  A VFD can hold a motor at any speed within its range, for as long as the process needs. A soft starter only smooths the transition to full speed. Once ramp-up finishes, the motor runs at line frequency, the same as if it started across-the-line.  2. Torque and Starting Behavior  VEIKONG’s hoist and crane drives show what a VFD can do that a soft starter can’t. Their frequency inverters use magnetic flux vector control technology, driven by a high-speed motor control DSP chip, to deliver high starting torque even at low frequency.   That precise, ongoing torque control is what lifting equipment needs for safety. A soft starter isn’t built for this. Its job is a smoother ramp-up, not ongoing torque management.  3. Energy Use in Variable-Load Applications  This is where a VFD offers savings a soft starter can’t match. VEIKONG’s pump application guide explains that when a frequency converter reduces a pump’s speed, the pump curve shifts down and the same flow is achieved at a lower pressure.   Lower pressure means longer seal life, less impeller wear, and less vibration and noise. Because of the affinity laws that govern pump and fan performance, power draw drops sharply as speed drops. That’s the basis for VFD energy savings in these systems.   A soft starter doesn’t touch running speed after startup, so it can’t unlock this kind of ongoing savings. Its value sits at the start of the motor cycle, not throughout it.  Typical Applications  Situation   Better fit  Pump or fan where flow needs to vary   VFD  Crane, hoist, or lifting equipment needing precise torque control   VFD  Process needing speed adjustments during operation    VFD  Compressor, crusher, or conveyor that just needs a gentler start    Soft starter   Fixed-speed motor where inrush current is the main concern   Soft starter   Budget-sensitive project where full speed control isn’t required    Soft starter   How to Decide  Does the process need different speeds, or just one? If speed changes during operation, choose a VFD. If the motor only runs at full speed once started, a soft starter may be enough. Is torque control critical, such as in lifting or precision work? Choose a VFD.   Is the main goal simply protecting the motor from the shock of a full-voltage start? A soft starter, like VEIKONG’s S6000, is a direct alternative to star-triangle or self-coupling decompression starters.   Are ongoing energy savings a priority, especially in pump or fan systems with variable loads? A VFD is built for that, since it can shift the pump curve and cut power draw as speed drops.  VEIKONG’s VFD and Soft Starter Lineup  VEIKONG manufactures both device types, making it easier to match the right equipment to the job without switching suppliers.  Variable Frequency Drives Include  Soft Starters Include   Why Motor Control Buyers Work With Veikong   Shenzhen VEIKONG Electric Co., Ltd. has specialized in researching, manufacturing, and trading high-, medium-, and low-voltage frequency inverters since 2004, giving the company more than 20 years of experience in product development and

Read More »
veikong

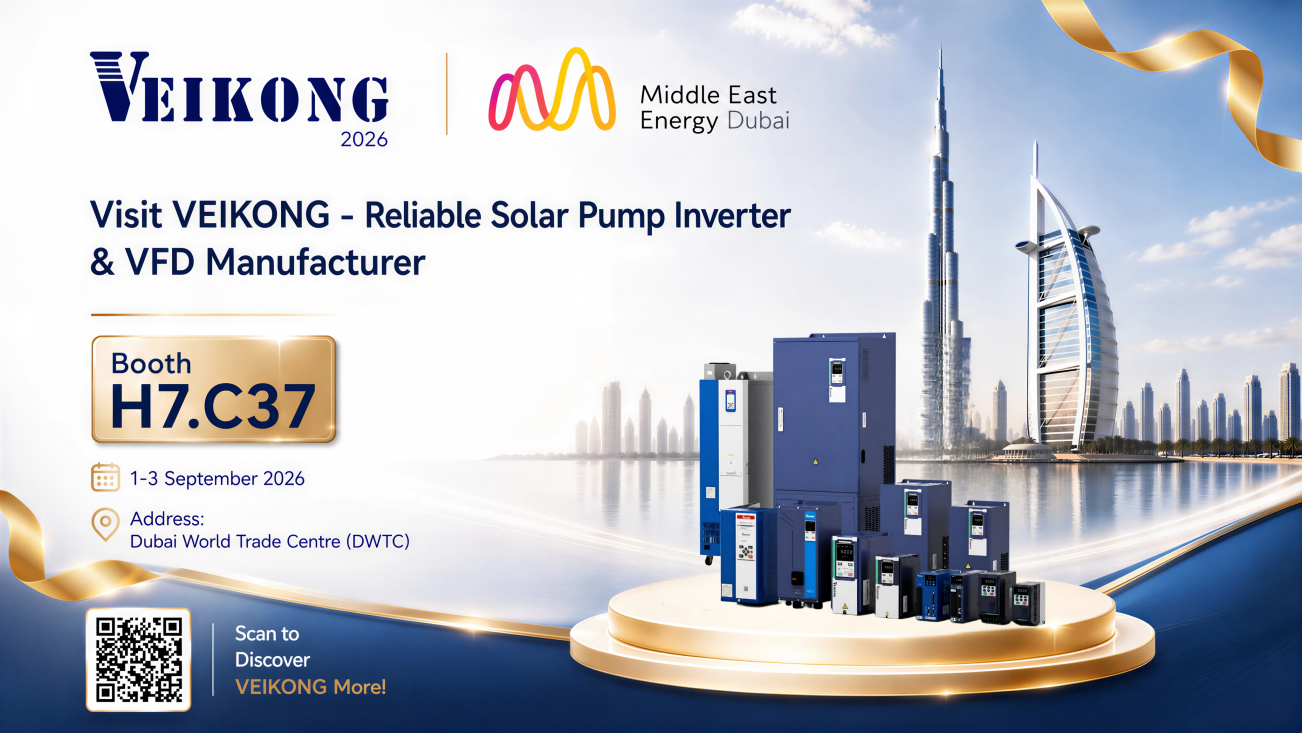
Meet VEIKONG at Middle East Energy Dubai 2026: Solar Pump Inverters and VFD Solutions at Booth H7.C37

VEIKONG warmly invites customers, distributors, engineering companies, and industry professionals to visit us at Middle East Energy Dubai 2026 from 1 to 3 September. Meet our team at Booth H7.C37 at the Dubai World Trade Centre and explore our reliable solar pump inverters, variable frequency drives, and industrial motor control solutions. Event Information Exhibition: Middle East Energy Dubai 2026 Date: 1–3 September 2026 Venue: Dubai World Trade Centre, Dubai, UAE VEIKONG Booth: H7.C37 As a professional manufacturer of solar pump inverters and variable frequency drives, VEIKONG looks forward to presenting practical solutions for solar-powered water pumping, industrial automation, motor speed control, and energy-efficient equipment operation. Discover VEIKONG Solar Pump Inverter Solutions Solar water pumping is becoming increasingly important in agriculture, livestock farming, residential water supply, and remote areas where grid power is unstable or unavailable. A suitable solar pump inverter helps convert solar energy into controlled motor power, enabling a water pump to operate efficiently under changing sunlight conditions. At Middle East Energy Dubai 2026, visitors can learn more about VEIKONG solar pump inverter solutions for irrigation, groundwater extraction, water storage, and other pumping applications. Our team will be available to discuss different power ratings, input voltage requirements, pump types, installation environments, and system configurations. For customers developing solar water pumping projects in the Middle East, Africa, Asia, and other regions, the exhibition provides an excellent opportunity to communicate directly with VEIKONG about project requirements. Whether you are planning a new system or upgrading an existing installation, our team can help you evaluate a suitable inverter solution based on the solar array, motor parameters, water demand, and operating conditions. Explore Reliable VFD Solutions for Industrial Applications VEIKONG will also introduce its variable frequency drive solutions for industrial motor control. A VFD adjusts the frequency and voltage supplied to an AC motor, allowing users to control motor speed according to actual process requirements. Proper VFD control can support smoother motor starting, more stable speed regulation, reduced mechanical impact, and improved energy efficiency. VEIKONG VFD solutions can be considered for applications such as pumps, fans, air compressors, conveyors, lifting equipment, winding systems, and industrial production machinery. Different applications require different control functions. A simple pump or fan may focus on energy-efficient speed adjustment, while a conveyor, crane, compressor, or production line may require stronger starting torque, faster response, coordinated control, or additional communication functions. At Booth H7.C37, visitors can discuss their motor data, load characteristics, control requirements, and site conditions directly with the VEIKONG team. Meet VEIKONG and Discuss Your Projects Face to Face An exhibition is more than a place to see products. It is also an opportunity to exchange technical ideas, understand local market needs, and develop long-term cooperation. During Middle East Energy Dubai 2026, the VEIKONG team welcomes discussions with distributors, system integrators, machine manufacturers, contractors, and end users. Visitors can bring motor nameplate information, application details, technical specifications, or project drawings to the booth for a more focused discussion. For potential distributors and business partners, VEIKONG will also be pleased to introduce our product range, application experience, technical support, and cooperation opportunities. We hope to understand the needs of different markets and build reliable partnerships with companies seeking professional solar pump inverter and VFD solutions. Visit VEIKONG at Booth H7.C37 If you are looking for a reliable solar pump inverter manufacturer, a variable frequency drive supplier, or a motor control solution for your next project, visit VEIKONG at Middle East Energy Dubai 2026. Join us from 1 to 3 September 2026 at the Dubai World Trade Centre. Our team will be waiting for you at Booth H7.C37 to introduce VEIKONG products, answer your technical questions, and discuss how our solutions can support your applications. We look forward to meeting you in Dubai and exploring new possibilities for energy-efficient water pumping and industrial motor control.

Read More »
Mechanical Resonance in Motor Systems

What Causes Mechanical Resonance in Motor Systems

What Causes Mechanical Resonance in Motor Systems and How Can Skip Frequency Control Help? Unexpected vibration and noise do not always mean that a motor or variable frequency drive is faulty. In some industrial machines, the equipment may operate smoothly at most speeds but begin to shake, hum, or vibrate strongly within a particular speed range. Once the motor passes that range, the vibration may decrease again. This behavior is often related to mechanical resonance. Understanding why resonance occurs and how VFD skip frequency control works can help engineers reduce vibration, protect mechanical components, and improve equipment reliability. What Is Mechanical Resonance? Every mechanical structure has one or more natural frequencies. These depend on factors such as mass, stiffness, shape, mounting method, shaft length, coupling design, and supporting structure. When an external force repeatedly excites a machine at or near one of its natural frequencies, the vibration can become much stronger. This effect is called mechanical resonance. In a motor-driven system, the excitation may come from rotating imbalance, shaft misalignment, couplings, fans, belts, gears, pumps, bearings, or the driven machine itself. A small vibration that is acceptable at one speed may become severe when the excitation frequency approaches the natural frequency of the mechanical system. For example, a fan may operate smoothly at 30 Hz and 45 Hz but show significant vibration around 38 Hz. The motor may not be overloaded, and the VFD may not report a fault. The problem appears because that operating point excites a resonant frequency in the fan, frame, duct, or mounting structure. How Does Motor Speed Affect Resonance? A variable frequency drive controls motor speed by changing its output frequency. As the frequency increases, the motor and connected machine pass through a wide range of rotational speeds. This flexibility improves process control, but it also means the equipment may enter a speed range that was rarely reached during fixed-speed operation. If that speed corresponds to a mechanical resonance point, vibration and noise may increase. The relationship is not always one-to-one. Gear mesh frequency, blade-passing frequency, belt vibration, motor harmonics, and other forces can also excite the machine. Therefore, the frequency displayed by the VFD should be treated as an operating reference rather than the only possible cause of vibration. What Is Skip Frequency Control? Skip frequency control, also called jump frequency or dangerous frequency avoidance, allows the VFD to avoid continuous operation within selected frequency bands. After a resonance range is identified, the technician can set a lower and upper limit around it. When the frequency command passes through this range, the VFD moves to the next permitted operating frequency instead of remaining at the resonant point. For example, if strong vibration occurs between 37 Hz and 39 Hz, the skip frequency range may be configured around that area. If the operator gives a command within the prohibited band, the drive will operate at an allowed frequency outside it, depending on the control logic and frequency direction. The motor may still pass briefly through the skip range during acceleration or deceleration. The purpose is to prevent the machine from operating continuously at the frequency that produces excessive vibration. How Should a Skip Frequency Range Be Set? Skip frequency settings should be based on actual testing rather than guesswork. During commissioning, the motor speed can be increased gradually while technicians monitor vibration, noise, current, bearing condition, and machine behavior. Once the problematic frequency range is identified, a narrow skip band can be set around it. The machine should then be tested again under real load because changes in material, pressure, tension, installation conditions, or mechanical load may affect the resonance point. The skip range should not be made unnecessarily wide. A large prohibited range may limit process control or prevent the machine from reaching an important operating speed. Acceleration and deceleration settings should also be reviewed so the system can pass through the resonance area smoothly without creating excessive mechanical shock. Can Skip Frequency Control Fix Every Vibration Problem? Skip frequency control is a useful operating tool, but it is not a substitute for mechanical maintenance. If vibration is caused by damaged bearings, loose bolts, poor foundations, worn couplings, rotor imbalance, shaft misalignment, or incorrect installation, avoiding one speed range will not repair the underlying problem. These faults may become worse and eventually affect other operating speeds. The machine should therefore be inspected before relying on frequency avoidance. If the required production speed falls directly inside the resonance range, a mechanical solution may be necessary. Possible measures include balancing rotating parts, correcting alignment, reinforcing the structure, changing mounting stiffness, adding damping, or redesigning the transmission system. Using VEIKONG VFD500 for Frequency Avoidance VEIKONG VFD500 includes dangerous frequency avoidance, making it suitable for compact industrial machines that need to avoid specific resonant operating speeds. Its adjustable acceleration and deceleration functions can help the motor move through sensitive speed ranges more smoothly. The VFD500 also supports V/F control and sensorless vector control, allowing the control method to be selected according to the motor and load. With standard Modbus communication, built-in braking units, multiple protection functions, and a compact structure, it can be considered for textile machinery, printing and packaging equipment, food machinery, plastic machinery, woodworking equipment, logistics systems, and other motor-driven applications. When applying VEIKONG VFD500, engineers should first identify whether the vibration is related to a particular operating frequency or a mechanical defect. With correct inspection, parameter setting, and load testing, the skip frequency function can help the machine avoid harmful resonance areas and maintain more stable operation.

Read More »
New VEIKONG CH530 Crane Drive

New VEIKONG CH530 Crane Drive: Built for Safer, Smarter and More

In lifting applications, a variable frequency drive must do much more than adjust motor speed. It must coordinate the mechanical brake, provide sufficient torque at low and zero speed, reduce load swing, respond to changing loads, and keep every lifting and travelling movement stable. Developed around these real operating challenges, VEIKONG has officially launched the new CH530 Series Crane Drive. Integrating professional brake sequence control, intelligent anti-slip technology, trolley and bridge anti-sway control, zero-servo support, and automatic speed adjustment according to load, the CH530 provides a specialized drive solution for modern lifting equipment. The new VEIKONG CH530 crane variable frequency drive supports asynchronous motors and permanent magnet synchronous motors. With a power range from 0.75 kW to 710 kW and three-phase 380–480 V input, it can be configured for a wide range of cranes, hoists and material handling systems. Safer Starting and Stopping with Professional Brake Control For a crane, starting and stopping are critical operating stages. If the mechanical brake opens before the motor develops sufficient torque, the suspended load may slip. If the brake closes at the wrong time, the equipment may experience mechanical shock, unstable movement or excessive wear. The CH530 integrates professional brake sequence control developed specifically for lifting equipment. The drive monitors output frequency and current before releasing or applying the mechanical brake. Adjustable delays help coordinate motor torque with brake action during both starting and stopping. Under closed-loop vector control, the CH530 can establish pre-torque before the brake is released, supporting a smoother transition from load holding to motor operation. This helps reduce load slipping and improves starting stability, especially in demanding hoisting applications. Strong Low-Speed Torque and Intelligent Anti-Slip Control Hoists, cranes and lifting mechanisms often need high torque before the motor reaches normal operating speed. A general-purpose speed control solution may not provide the response required when starting a heavy suspended load. The VEIKONG CH530 features an intelligent anti-slip algorithm and can provide starting torque of at least 150% under the appropriate vector control configuration. This enables the motor to produce useful torque at low or zero speed and supports stable operation during lifting and lowering. The integrated zero-servo function provides additional operational support. If the mechanical brake is delayed or its braking force is insufficient, the drive can detect motor shaft movement while the system is powered, attempt to hold the mechanism at its current position, and activate an alarm. These functions support the crane safety system but do not replace the mechanical brake, limit protection or other safety devices. The drive, motor, brake and crane control system must be correctly selected and commissioned as one complete system. Reduce Load Swing and Improve Positioning Efficiency Load swing is a common challenge in crane operation. It can slow down material handling, increase positioning difficulty and require additional time before the next movement can begin. The CH530 integrates anti-sway control for trolley and bridge travel. By optimizing acceleration and deceleration, the drive helps reduce load swing during crane movement and supports faster, more stable positioning. Linear and S-curve acceleration and deceleration are available, together with four adjustable ramp-time groups. These settings allow different operating profiles to be configured for hoisting, trolley travel, bridge travel and tower crane slewing. Automatic Speed Adjustment According to Load A crane does not operate under the same load during every working cycle. Empty or lightly loaded travel can often run faster, while heavy loads require more controlled movement. The CH530 can automatically increase operating speed under light-load conditions to improve working efficiency. When a heavy load or overload condition is detected, the drive can reduce speed to support stable operation and reduce stress on the motor and mechanical system. This load-based speed adjustment helps crane users balance productivity, equipment protection and operational stability without relying on one fixed speed for every working condition. Simpler Commissioning for Different Crane Motors Crane upgrade and replacement projects often involve motors from different manufacturers. The CH530 supports asynchronous motors, permanent magnet synchronous motors and cone motors, making it suitable for both new equipment and retrofit projects. Its one-key motor identification function helps identify important motor and mechanical parameters, reducing the work required to match third-party motors. Built-in crane parameter macros also allow technicians to complete the basic configuration for common lifting applications more quickly. The CH530 comes with a standard LED keypad. Dual-display and color LCD keypads are available as options. The optional LCD keypad supports parameter backup, copying and file export, making it easier to manage multiple drives, share parameter files and provide remote commissioning support. Compact Design for Demanding Industrial Environments Compared with the previous generation, the CH530 uses a high-power-density design that reduces product volume by approximately 30%. The compact structure helps save control cabinet space and simplifies the electrical layout. Selected models up to 90 kW are available with built-in braking units, while higher-power models can work with external braking units. An independent cooling air duct helps prevent dust from entering sensitive internal areas, and high-airflow cooling fans support stable heat dissipation. The automatic conformal-coating process provides consistent protection for circuit boards, improving product adaptability in industrial environments involving dust, humidity, temperature changes and unstable power supplies. One Crane Drive for Multiple Lifting Applications The VEIKONG CH530 lifting equipment inverter can be applied to overhead cranes, gantry cranes, quay cranes, yard cranes, tower cranes, construction hoists, mine hoists and other material handling equipment. By combining professional brake control, high starting torque, anti-slip operation, anti-sway technology and automatic load-based speed adjustment, the CH530 addresses the key control requirements of modern crane systems. For crane manufacturers, system integrators and end users seeking a professional crane variable frequency drive, VEIKONG CH530 offers a flexible platform for both asynchronous and permanent magnet synchronous motor applications. Contact VEIKONG with your motor nameplate, lifting capacity, operating mechanism and control requirements, and our team will help you evaluate a suitable CH530 crane drive solution.

Read More »
VFD

10 Industries That Rely on Variable Frequency Drives (And Why)

Motors keep industrial operations moving, from pumps and fans to conveyors and mixers. Most of these motors don’t need to run at full speed all the time. That’s where a variable frequency drive, or VFD, becomes useful. Here’s what it does, in simple terms: a VFD changes the frequency of the electricity going into an AC motor, and that changes how fast the motor spins. Instead of a motor running flat-out whether the job calls for it or not, a VFD adjusts speed to match actual demand on the line. The result is less wasted energy, less wear on gears and bearings, and considerably more control than a standard on/off switch allows. So which industries rely on their technology day to day? Quite a few, and often for different reasons. Here is the list of 10 industries that rely on VFDs. 1. Oil and Gas Boiler fans in oil and gas plants tend to run nonstop; they don’t all need full airflow every hour of the day. Retrofitting induced-draft and forced-draft boiler fans with VFDs for energy savings is a fairly standard move in this sector, mostly because these fans log so many operating hours that even small efficiency gains add up fast. 2. Water Supply and Municipal Pumping Anyone who’s worked with municipal water systems knows demand isn’t flat. It climbs in the morning, drops off overnight, and spikes without warning when something goes wrong elsewhere in the network. A VFD on a water pump adjusts motor speed to track that actual demand curve, rather than running the pump at one constant rate and throttling a valve to compensate, which simply burns extra power for nothing. Multi-pump control panels take it further by coordinating several pumps together, rotating which unit carries the load so one motor doesn’t wear out faster than the rest of the fleet. 3. Agriculture and Solar Water Pumping Out in remote farmland, the power grid often isn’t reliable, or isn’t there at all. Solar-powered water pumps have filled that gap for irrigation and livestock water supply. The same setup scales up nicely for bigger water projects too, including irrigation basins and public swimming facilities that need a steady, sizable water supply. 4. Manufacturing and Compressed Air Systems Compressed air runs half of what happens on a factory floor: tools, packaging equipment, pneumatic controls. And air compressors have a bad habit of wasting energy when they’re built to run at full output, but the plant only needs a fraction of that. Add a VFD, and the compressor reads pressure from a remote sensor and adjusts motor speed to hold that pressure right where it needs to be. Say a plant needs 0.76 MPa. The drive keeps things sitting at that number instead of overshooting and venting the excess. That precision alone cuts a surprising amount of wasted energy, and it’s easier on the compressor’s internals too. 5. Material Handling: Hoists and Cranes Lifting something heavy safely comes down to torque control, and the first few seconds of a lift are usually where things go wrong if they’re going to. Ports, warehouses, and construction sites- anywhere cranes and hoists are working- all lean on this kind of torque and speed management. 6. Plastics and Injection Molding Most injection molding machines still run on hydraulic power, but the pump behind the hydraulics doesn’t actually need to spin at one fixed speed the whole way through a molding cycle. Fitting a VFD lets pump speed track each stage separately: fast during mold filling, slower during cooling, adjusted again for ejection. That alone trims electricity use and cuts down on heat buildup in the hydraulic fluid, which means the seals and valves last longer before needing replacement. 7. Plastic Disk Molding Disk-type plastic molding machines throw sudden, sharp load changes at their motors mid-operation. A standard motor takes that kind of shock poorly, and it shows up as shortened service life. 8. Textiles and Building Materials Textile mills and building material plants each run a small army of motors, including winders, mixers, extruders, and conveyors, often all at different speeds within the same shift. VFDs let every motor run at whatever speed its particular job calls for, rather than forcing one fixed rate across an entire production line. In textiles, that means tension stays consistent through the fabric. In cement or brick production, it keeps mixing and extrusion steady and repeatable. Both industries pick up an added bonus too: lower starting current, since a VFD ramps motors up gradually instead of hitting them with full power right away. 9. Power Generation and Electric Utilities Power plants and utilities run large fans, pumps, and auxiliary equipment that all need to respond as load conditions shift, sometimes hour to hour. 10. Home Appliances: Washing Machines Even the washing machine in a laundry room uses this same principle. A wash cycle isn’t one speed. It runs through several, back to back. Fill, wash, rinse, and spin each call for a completely different drum speed, and the gentle motion needed for washing has nothing in common with the speed needed for a fast spin-dry. A variable frequency drive handles the whole cycle with a single motor, adjusting speed as each stage arrives. That’s a far simpler, more efficient approach than building in separate motors or gear assemblies for every stage. How Veikong Electric Supports Industries with Reliable Variable Frequency Drives Shenzhen Veikong Electric Co., Ltd. has been building AC drives and VFDs for more than 20 years now, and honestly, its product line touches most of the industries covered above. The drives themselves run on SPWM and sensorless vector control technology, and the company holds ISO9001 and CE certification across its manufacturing and quality processes. Veikong describes its products as a direct equivalent to established European, American, and Japanese drive brands, giving buyers a comparable option with technical support behind it. Choosing the Right VFD for Your Industry No two industries have quite the same need from a drive. A crane wants strong

Read More »
VFD

Why Low Speed High Torque Performance Matters in Industrial Motor Applications?

Motor speed is easy to see, but torque often decides whether an industrial machine can start and run smoothly. Torque is the turning force at the motor shaft. Even at low speed, a machine may need torque to overcome friction, gravity, material weight, process resistance, or inertia. A drive that maintains useful torque at low speed is important in many applications. This requirement differs from simple fan and pump duty. Centrifugal fans and pumps normally need less torque as speed decreases. Conveyors, mixers, extruders, winding machines, crushers, and hoists may have a constant torque load. If the motor cannot develop enough torque, the machine may stall, accelerate slowly, lose process stability, or overload the drive. Why Basic Speed Control May Not Be Enough? Basic volts per hertz control changes output voltage and frequency together. It can work well for variable torque loads, but it may have limits at low speed. At low output frequency, voltage drop in the motor stator becomes more significant. If magnetic flux is not maintained correctly, the motor may produce less torque and more heat. A torque boost setting can improve starting performance, but it must be used carefully. Too little can leave the motor weak, while too much can increase current and temperature. For demanding loads, vector control is often a better approach. It regulates motor current and separates the current associated with magnetic flux from the current associated with torque. This helps the drive respond accurately to load changes. Sensorless vector control can provide good low speed torque and speed regulation in many applications without an encoder. Closed loop vector control uses encoder feedback and may be selected when the machine needs accurate speed, strong torque near zero speed, positioning, or controlled response. The right choice depends on the motor type, load, and requirement. Where Low Speed Torque Matters? A loaded conveyor may need to start gradually yet still produce enough torque to move the full load. Mixers and extruders can experience high resistance when material becomes thicker or when the process starts from rest. In winding and unwinding equipment, stable torque helps maintain material tension as roll diameter changes. Hoists and lifting equipment require special care. The drive must coordinate with the mechanical brake and control system so the load is held and moved safely. A VFD should not be treated as the only safety device. The motor, braking system, limit protection, and control sequence must be designed as one system. Reliable low speed torque can support smoother acceleration, reduce mechanical shock, prevent stalls, and improve process consistency. Motor Cooling and Drive Sizing Low speed operation creates a thermal challenge. Many standard motors use a shaft mounted cooling fan. When the motor slows down, the fan also slows down. A motor delivering high torque for a long period at low speed can generate heat faster than it removes it. This may require an inverter duty motor, an independently powered cooling fan, a lower continuous torque limit, or a different mechanical design. Drive selection should be based on current and overload demand, not rated power alone. Engineers should review rated current, starting torque, duty cycle, acceleration time, inertia, gearbox ratio, ambient temperature, altitude, and enclosure conditions. A drive sized only by kilowatts may be unsuitable if the machine requires frequent heavy starts or long duration torque at low speed. Commissioning and Protection Correct motor data is essential. Rated voltage, current, frequency, speed, power, connection method, and control mode should be entered accurately. Motor identification or auto tuning can help the drive build a better control model when the application allows it. During commissioning, users should test under real load and check current, temperature, vibration, ramp performance, and alarms. Torque limits can help prevent mechanical overload, while acceleration and deceleration settings can reduce stress on the machine. Vertical or high inertia loads may return energy to the drive during deceleration, so braking requirements should be assessed before full duty operation. For industrial projects that need low speed torque performance, VEIKONG VFD530 can be evaluated for PMSM and induction motor applications. Its configuration should be chosen according to motor type, load profile, current requirement, speed range, and feedback needs. The final selection should also consider the mechanical system and site conditions. Low speed high torque performance is not a single number on a datasheet. It results from matching the motor, drive control mode, cooling method, overload capacity, gearing, and commissioning process to the real machine. When these elements are selected together, a VFD can provide more reliable motion and better process control at the speeds where the work is often hardest.

Read More »